Choosing a Tube Fiber Laser: Comparing Material, Work Envelope, and Automation Trade-offs
Framing the decision
Picking a machine means weighing choices, not chasing specs. Think of a tube laser cutting system as a toolbox: some tools are precise for thin stainless, others brute-force thick carbon steel. The Comparative Insight approach here lines up common pairings—material versus power, work envelope versus throughput, manual loading versus automated cells—so you can see what you gain and what you give up before a purchase.
Material match: what the metal demands
Aluminum, stainless, mild steel and coated tubes behave differently under a focused fiber beam. For thin-walled stainless (≤6 mm) a 1 kW class source gives fast, clean edges; for thicker carbon steel you need 2–4 kW to avoid slow feed rates and excessive heat input. Coated or painted tubes require pre-cleaning or higher assist gas control to stop slag. Choose for the thickest, most-difficult profile you expect to cut frequently—otherwise you’ll throttle every job.
Work envelope and geometry: diameter, length, and complexity
Small-diameter runs and long bars push different requirements. If you cut 6–20 mm OD furniture spindles, a compact chuck with a rotating collet and short travel wins for cycle time. If you handle 120 mm OD structural tubes or 6 m lengths, you need a larger bed, multi-chuck stages or an infeed/outfeed handling system. Oval, tapered or internally profiled tubes demand flexible clamping and more sophisticated CNC compensation; underestimate geometry and you’ll fight alignment and scrap rates.
Automation trade-offs: throughput versus flexibility
Automation raises throughput but narrows flexibility. Bar feeders and automatic loaders dramatically reduce cycle time for high-volume runs, yet they require repeatable part sizes and committed production flows. Manual loading gives immediate adaptability for prototypes or mixed batches but increases labor cost per part. Compare takt time: if your daily demand supports continuous runs, automated feeding offsets capital quickly; if you run varied prototypes, leave room to keep an operator in the loop.
Control systems, nesting and operator skill
Software matters as much as optics. Advanced nests that handle bevels, multi-segment tubes, and pierce sequencing shorten setups. Some controllers provide adaptive feed based on real-time cut quality, others rely on fixed tables. A less experienced operator can still produce quality parts with better software and guarded defaults; conversely, seasoned operators can coax higher throughput from simpler systems. Plan training alongside purchase—software shortcuts are where real daily gains appear.
Service, spares and the real cost of ownership
Laser sources, protective lenses, nozzles and gas usage define recurring costs. A cheaper machine with long lead times for spare optics will cost you days of downtime; a well-supported platform with local service minimizes lost shifts. Warranty terms, onsite diagnostics, and local parts inventory matter. Buy with an eye on realistic maintenance intervals and transparent consumable pricing—those figures decide whether your price-per-part is competitive next quarter.
Common mistakes buyers make
1) Buying on peak power alone and ignoring beam quality—higher kW with poor focus still makes bad cuts. 2) Choosing minimal automation for a projected growth profile—retrofitting later is costly. 3) Overlooking handling for long tubes—transport damage and misalignment surface on day one. 4) Skimping on training—operator error creates variability that looks like machine fault. Avoid these and you save time and scrap.
Evidence from the floor and expert perspective
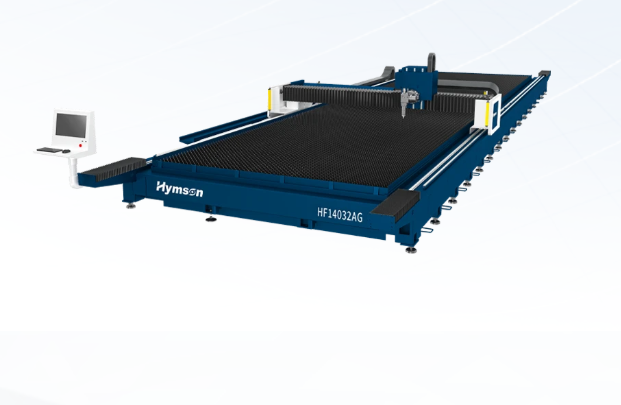
Coverage of trade shows and vendor demos, plus conversations with fabricators at Fabtech in Chicago, reveal consistent patterns: shops that matched machine class to their toughest material and planned handling for longest pieces ran leaner and had lower scrap. Based on field observations and tested setups, the typical shop benefits from a mid-range source with good beam quality and modular automation that scales. For direct equipment reference, the tested cnc tube laser cutter models show how those trade-offs are implemented on modern platforms—power options, rotators, and loader choices are the levers you’ll actually use on the floor.
Final synthesis
Compare options by asking three clear questions: what material and thickness are most frequent, what part sizes define your work envelope, and how stable is your production schedule. Answer these, and you’ll know whether to prioritize beam quality, bed size, or an automated cell. The result is a machine choice grounded in daily reality and service expectations—an outcome I’ve seen realized repeatedly with experienced manufacturers such as Hymson.